Explore our top-tier medical furniture, patient transfer systems, and mobility accessories built to international healthcare standards.

Analyzing the macroeconomic and clinical shifts driving the demand for specialized, adjustable, and custom-manufactured wheelchairs.
Modern clinical healthcare environments demand seating systems that accommodate varying physical pathologies. Adaptable wheelchairs designed with modular frame geometry enable swift adjustments in center-of-gravity, seat-to-floor height, backrest angle, and axle position without requiring structural frame modifications.
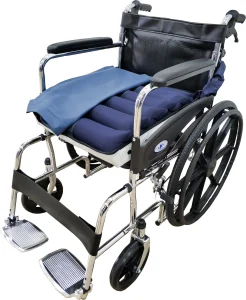
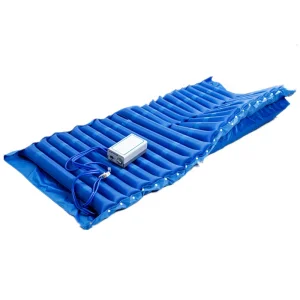
Preventing secondary musculoskeletal deformities and pressure ulcers is paramount. OEM manufacturing now integrates dynamic seating dynamics, anti-decubitus air cushions, microclimate management fabrics, and anatomically sculpted posture supports into standard adaptable wheelchair chassis.
Global medical device procurement mandates strict compliance with ISO 7176 dynamic fatigue standards, EN ISO 13485 quality systems, FDA 510(k) registrations, and European CE MDR regulations. Custom wheelchair exporters must guarantee total traceability across raw material supplies.
Clinical Insight: Research indicates that customizable wheelchair configurations reduce long-term caregiver stress by 42% and decrease user tissue ischemia risks by up to 65% through optimal weight redistribution and dynamic posture tuning.
Hengshui Zenith Medical Co., Ltd. is a leading manufacturer specializing in the production of hospital beds, home care beds, air mattresses, hospital furniture, and a range of related medical equipment. Our company is committed to improving the quality of life for patients and the elderly, offering products that ensure comfort, safety, and reliability. With a focus on high-quality manufacturing, we strive to meet the ever-evolving needs of the healthcare industry while adhering to the highest standards of excellence.
At Hengshui Zenith Medical, quality is at the core of everything we do. Our production process starts with precision in the selection of raw materials and the meticulous welding of product structures. We take stringent measures to ensure the superior finish of each product, including rigorous quality checks on spraying processes. Our advanced manufacturing equipment, such as laser cutting machines and robotic welding systems, allows us to maintain exceptional standards of precision and consistency.
Our Research and Development (R&D) department works tirelessly to innovate and enhance our product offerings. We continuously introduce new products that are designed to meet the evolving needs of our customers, incorporating feedback from both the market and our global network of distributors.
We turn complex clinical requirements into mass-producible, highly durable mobility hardware.
Our engineering teams utilize high-tensile 7005/7075 aircraft-grade aluminum alloy, ultra-light carbon fiber composites, and surgical stainless steel. Frame tubing undergoes multi-pass TIG robotic welding and heat treatment (T6 tempering) to guarantee structural rigidity while minimizing total tare weight. Customizable chassis parameters include adjustable camber angles (0° to 6°), extension depth, telescoping footrests, and heavy-duty reinforced cross-bracing for bariatric applications (up to 250kg dynamic weight rating).
For hybrid and motorized adaptable wheelchairs, we design seamlessly integrated electro-mechanical drive systems. Incorporating high-torque brushless DC (BLDC) hub motors, electromagnetic braking units, precision planetary gearboxes, and CAN-bus intelligent controller interfaces. Power options support fast-charging lithium iron phosphate (LiFePO4) battery packs with integrated Battery Management Systems (BMS) for enhanced range, thermal stability, and air travel safety compliance.
Tailored supply-chain partnerships for medical distributors, hospital conglomerates, and government tenders.
High-turnover clinical settings require heavy-duty, easily sanitizable, and quickly adjustable mobility equipment. Our standard and customizable hospital transport chairs and adaptable wheelchairs feature antimicrobial polyurethane upholstery, sealed precision bearings, and integrated IV pole mounts for continuous hospital ward utility.
Therapy facilities demand specialized seating with precise anthropometric customization. We provide OEM solutions with fine-tunable tilt-in-space mechanisms, elevating legrests with knee axis alignment, and specialized harness accessories to support comprehensive neuro-rehabilitation therapy.
Retail and homecare distributors benefit from our compact, foldable chassis designs that maximize shipping container density and simplify home storage. Ergonomic folding backrests, quick-release rear wheels, and tool-free height adjustment minimize total landed logistics costs and end-user setup complexity.
Hengshui Zenith Medical's commitment to quality is reflected in our compliance with international standards. We hold ISO 9001:2015 and EN ISO 13485:2016 certifications, ensuring that our products meet the highest levels of quality, safety, and efficiency. Each product undergoes thorough testing and inspection before it reaches our customers, guaranteeing that it meets both functional and safety requirements.
Our company has successfully expanded its market reach across Asia, Southeast Asia, the Middle East, South America, and various other international markets. We have established strong, long-term partnerships with distributors around the world. These relationships have played a crucial role in enhancing our brand presence and market share. Through open communication with our partners, we gain valuable insights into market trends and product optimization, which helps us develop better and more efficient solutions.
Our global expansion is driven by our dedication to offering excellent after-sales services. We pride ourselves on our responsive customer support, offering quick solutions to any issues our clients may face. Our team is always available to ensure that our products are functioning optimally and to assist in resolving any challenges that may arise.
Hengshui Zenith Medical's mission is to provide the highest quality products, comprehensive services, and solutions that contribute to the well-being and happiness of patients and the elderly. We aim to support healthcare providers, caregivers, and families in improving the quality of life for those in need of medical and home care.
Our vision is to be a global leader in the healthcare equipment industry, providing advanced, reliable, and innovative products that make a positive impact on people's lives. We are dedicated to helping our customers succeed in an increasingly competitive market by delivering top-tier products and exceptional service.
Integrating artificial intelligence, IoT telematics, and advanced smart materials into modern wheelchair manufacturing.
Incorporating IoT sensors directly into hospital wheel assets to track location, user posture data, seat pressure dynamics, and component wear in real-time for automated preventive maintenance.
Developing Bluetooth and mobile app-connected air cushions with dynamic micro-pumps (like our APP Wheelchair Cushion series) that cycle inflation zones autonomously to prevent decubitus ulcers.
Pioneering eco-friendly manufacturing using recycled magnesium alloys and thermoplastic composite frames that achieve superior tensile strength with a 30% reduction in total structural weight.
Detailed answers regarding manufacturing customization, compliance standards, order minimums, and global logistics.
Discover our comprehensive array of anti-bedsore pressure solutions, medical trolleys, monitor mounts, and patient lift devices.

 Zenith Medical