Aota202 Carbon Fiber Surgical Operation Table Extension Device Orthopedic Traction Frame for Various Positions
View Details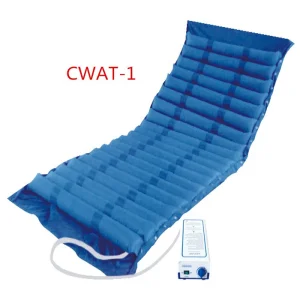
Alternating Pressure Ulcer Prevention and Therapy Anti Decubitus Bedsore Air Inflatable Mattress
View Details
Transfer Board for Hemiplegia & Disabled Elderly Care Wheelchair & Bed Transfer Device with Lower Limb Support
View DetailsHengshui Zenith Medical Co., Ltd. is a leading manufacturer specializing in the production of hospital beds, home care beds, air mattresses, hospital furniture, and a range of related medical equipment. Our company is committed to improving the quality of life for patients and the elderly, offering products that ensure comfort, safety, and reliability. With a focus on high-quality manufacturing, we strive to meet the ever-evolving needs of the healthcare industry while adhering to the highest standards of excellence.
Backed by decades of engineering expertise, our infrastructure is designed to deliver uncompromised safety rails and support systems that comply with rigorous international healthcare mandates. We bridge the gap between advanced clinical requirements and practical, scalable manufacturing.
At Hengshui Zenith Medical, quality is at the core of everything we do. Our production process starts with precision in the selection of raw materials and the meticulous welding of product structures. We take stringent measures to ensure the superior finish of each product, including rigorous quality checks on spraying processes.
Our advanced manufacturing equipment, such as laser cutting machines and robotic welding systems, allows us to maintain exceptional standards of precision and consistency across every safety rail and medical bed chassis we fabricate.
Our Research and Development (R&D) department works tirelessly to innovate and enhance our product offerings. We continuously introduce new products that are designed to meet the evolving needs of our customers, incorporating feedback from both the market and our global network of distributors.
Demonstrates our robust quality management systems, ensuring consistent design, manufacturing, and customer service performance across our entire product portfolio.
Represents our stringent adherence to international regulatory requirements specifically tailored for medical device manufacturing and risk management protocols.
Each product undergoes thorough testing and inspection before it reaches our customers, guaranteeing that it meets both functional and safety requirements under extreme conditions.
Our company has successfully expanded its market reach across Asia, Southeast Asia, the Middle East, South America, and various other international markets. We have established strong, long-term partnerships with distributors around the world. These relationships have played a crucial role in enhancing our brand presence and market share.
Leveraging China's world-class industrial ecosystem, our supply chain ensures unmatched cost efficiency without compromising material integrity. Through open communication with our partners, we gain valuable insights into market trends and product optimization, helping us develop superior solutions.
Our global expansion is driven by our dedication to offering excellent after-sales services. We pride ourselves on our responsive customer support, offering quick solutions to any issues our clients may face. Our team is always available to ensure that our products are functioning optimally.
Hengshui Zenith Medical's mission is to provide the highest quality products, comprehensive services, and solutions that contribute to the well-being and happiness of patients and the elderly. We aim to support healthcare providers, caregivers, and families in improving the quality of life for those in need of medical and home care.
Our vision is to be a global leader in the healthcare equipment industry, providing advanced, reliable, and innovative products that make a positive impact on people's lives. We are dedicated to helping our customers succeed in an increasingly competitive market by delivering top-tier products and exceptional service.
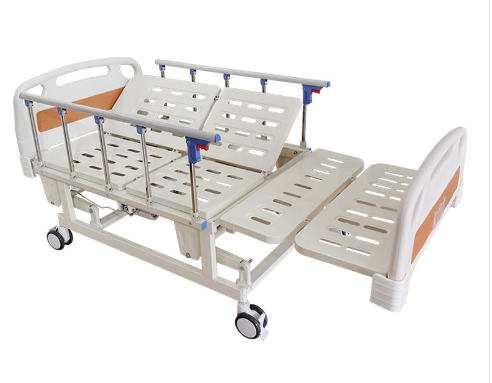
Our manufacturing facility operates under strict quality management frameworks, holding ISO 9001:2015 and EN ISO 13485:2016 certifications. Every batch of safety rails and medical furniture undergoes rigorous load-bearing and fatigue testing prior to shipment.
Yes, we specialize in OEM and ODM partnerships. We work closely with global distributors to tailor product dimensions, branding, packaging, and specific functional specifications to meet local regulatory and market demands.
We have established long-term supply relationships across Asia, Southeast Asia, the Middle East, South America, and various European nations, ensuring reliable logistics and responsive after-sales support worldwide.
By utilizing state-of-the-art automated manufacturing equipment, robust raw material stockpiling, and strategic transport partnerships, we maintain consistent production capacity and reliable lead times for large-scale B2B orders.
 Zenith Medical