Explore our top-tier manufacturing lines built to global healthcare and institutional standards.
A Global Authority in Healthcare Equipment Manufacturing and Smart Logistics Solutions
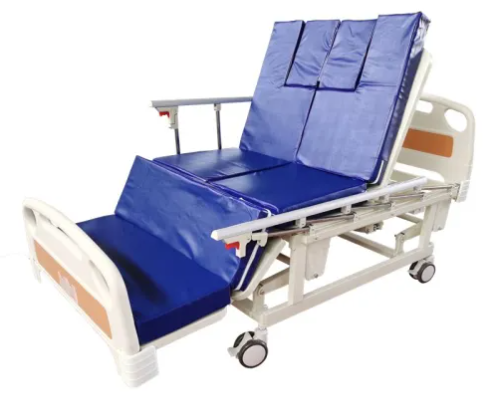
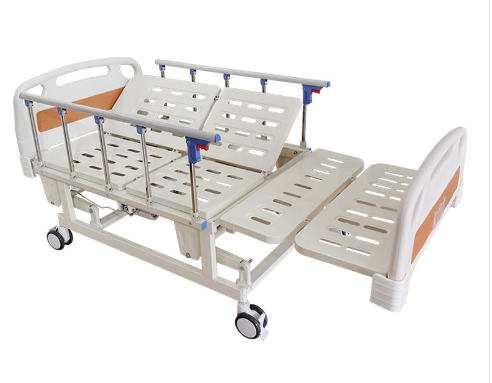
Hengshui Zenith Medical Co., Ltd. is a leading manufacturer specializing in the production of hospital beds, home care beds, air mattresses, hospital furniture, meal delivery carts, and a comprehensive range of related medical equipment. Our company is deeply committed to improving the quality of life for patients and the elderly, offering products that ensure absolute comfort, safety, and reliability.
With a strategic focus on high-quality manufacturing infrastructure, we continuously strive to meet the ever-evolving demands of the global healthcare and institutional catering industries while adhering strictly to international standards of excellence.
At Hengshui Zenith Medical, uncompromising quality forms the foundational core of our enterprise. Our end-to-end production workflow initiates with extreme precision in raw material selection, progressing through meticulous structural welding to finished product deployment.
We deploy state-of-the-art manufacturing equipment—including ultra-precise laser cutting machines and automated robotic welding systems—to maintain exceptional dimensional consistency and structural integrity across all meal delivery carts and hospital furniture units.
Our dedicated Research and Development (R&D) engineering team works tirelessly to innovate and upgrade product lines. By closely analyzing global market dynamics and direct user feedback from our extensive international distribution network, we consistently launch cutting-edge solutions tailored for modern healthcare operations.
Strategic insights into global institutional procurement and macro industry transformation.
China's industrial clusters offer unmatched supply chain integration for stainless steel processing, automated thermal insulation technology, and precision castors. This complete ecosystem enables top-tier factories like Zenith Medical to deliver robust meal delivery carts with superior cost-efficiency and rapid scalable production capacity.
The institutional catering sector is shifting rapidly toward smart temperature-controlled logistics, ergonomic mobility, and antimicrobial surfaces. Modern healthcare facilities and elderly care centers demand insulated meal distribution systems that guarantee food safety and optimal nutritional temperature over prolonged transit times.
Global enterprise buyers and hospital group purchasers require reliable OEM/ODM partners capable of navigating international regulatory compliance. Zenith Medical provides end-to-end customized logistics solutions, stringent pre-shipment quality verification, and robust after-sales technical backing to ensure frictionless global procurement.
Anchored in international compliance and dedicated to global well-being.
Our unwavering commitment to quality is formally verified through rigorous international standard compliances. We proudly hold ISO 9001:2015 and EN ISO 13485:2016 certifications. Every single product undergoes exhaustive multi-point testing before dispatch, guaranteeing absolute functional reliability, safety, and regulatory compliance for global markets.
Zenith Medical has successfully expanded across Asia, Southeast Asia, the Middle East, South America, and beyond. Our vision is to stand as the global benchmark in healthcare and institutional equipment, providing innovative, reliable solutions that empower our worldwide distribution partners to lead their respective regional markets.
Expert answers regarding our manufacturing capabilities, meal delivery carts, and partnership terms.
We combine over 15 years of medical equipment manufacturing expertise with advanced laser cutting and robotic welding infrastructure. Our strict adherence to ISO 13485 standards ensures superior durability, thermal efficiency, and hygiene for all institutional meal transport equipment.
Yes! We specialize in OEM and ODM manufacturing partnerships. Whether you require specific dimensions, custom shelving configurations, or tailored branding for hospital projects, our R&D and engineering teams deliver fully customized solutions.
Our manufacturing facility and product lines are certified under ISO 9001:2015 and EN ISO 13485:2016, satisfying stringent international medical and institutional equipment regulatory requirements.
Every product undergoes rigorous multi-stage quality inspections before packaging. We utilize export-grade reinforced packaging materials and partner with reliable global logistics providers to ensure secure, damage-free delivery worldwide.
Explore our specialized medical trollies, transfer aids, and professional hospital furniture.
 Zenith Medical